PET bottles are currently the most mainstream product in the beverage packaging industry.
PET products are used on a large scale for the packaging of various foodstuffs because of their hardness, good toughness, high strength, bright appearance, environmental protection and non-toxicity, while bottle blanks are the primary products used to produce plastic bottles of various shapes and capacities.
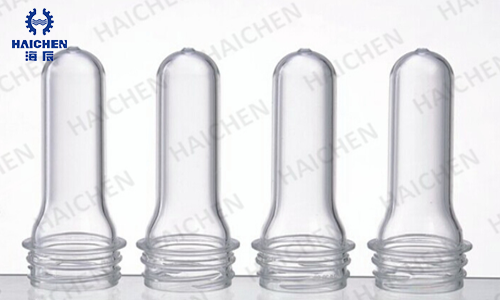
How many kinds of PET bottle preform ?
There are three kinds of PET bottle preform:Narrow mouth,wide mouth,Special large capacity.
Narrow mouth
25mm, 28mm, 30mm, 32mm, etc.
These products are mostly used for the production of small volume liquid bottles.
Wide mouth
50mm, 53mm, 63mm, 73mm, 83mm, 90mm, 96mm, etc.
Wide-mouth products are mostly used for cans for solid goods.
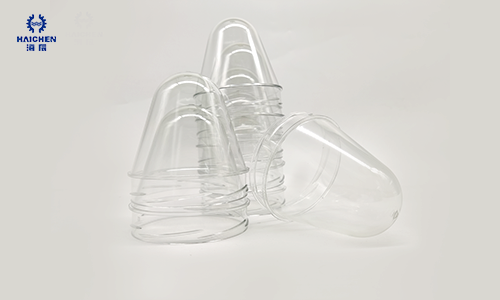
Special large capacity
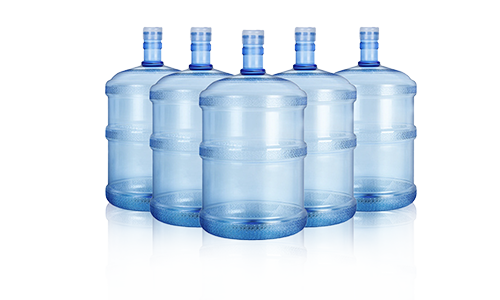
55mm calibre 3-5 gallon water bucket.
This is a large-capacity special preform commonly used in the drinking water industry.
Product characteristics
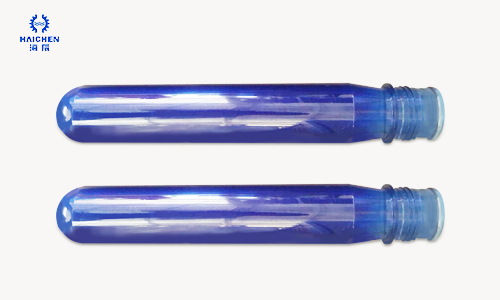
Narrow-mouth for the beverage industry
Narrow-mouth products are used in the beverage industry, mostly disposable products, with a large output demand.
And most of them are produced with pure PET material to ensure that the products are clean and non-toxic, without any adverse effects on the human body.
Wide mouth for solid goods
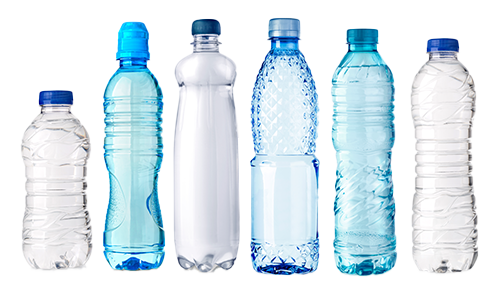
Wide mouth products in English for solid goods such as candy, snacks, pharmaceuticals, the requirements for colour are more varied than for beverage bottles, and customers often require the addition of different colouring agents to adjust the colour to increase the aesthetics of the packaging or to meet the requirements of certain drugs to be stored away from light.
Special large-capacity for barrels of water
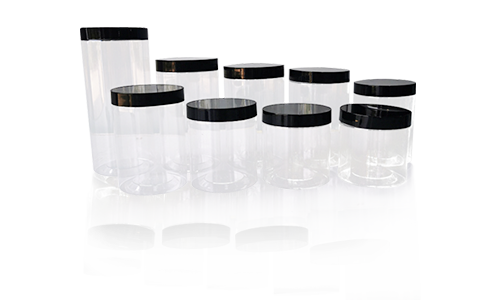
Special large-capacity bottles are used for the transfer of barrels of water, where the weight of the product is large and the final product must be recycled several times.
How to produce the PET bottle preform ?
Bottle preform, like all plastic products, are formed by injecting molten material into the mold through an injection molding machine.
However, according to the characteristics of PET materials, there are several special requirements during the production process.
Determine product parameters: caliber, weight, and production capacity
Firstly, determine the caliber size and weight of the product. Then determine the number of cavities according to production capacity requirements.
Noramlly we will need following details of bottle,then according those details to choose the mould and machine.
4 bottle elements, to help us selecting machines:
-Bottle preform neck size;
-Weight of bottle;
-Cavities of mould;
-Mold size
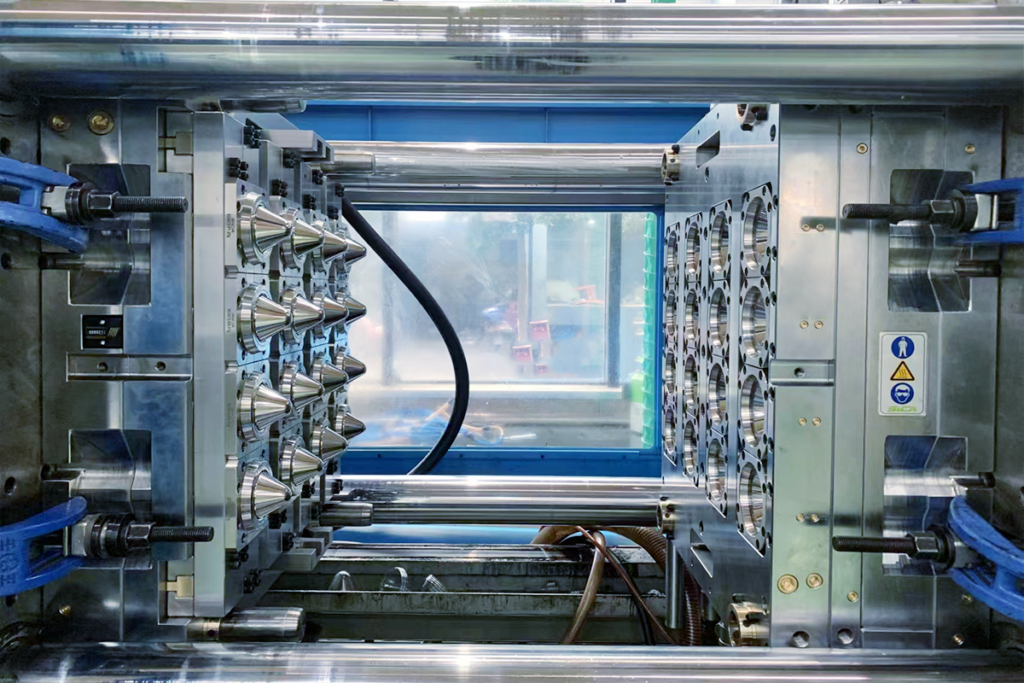
Mold selection and design
There are two type of PET bottle proform mould: Valve type mould and Self-locking type mould.
The bottle embryo mold production uses a hot runner. The mold is divided into needle valve type and self-locking type.
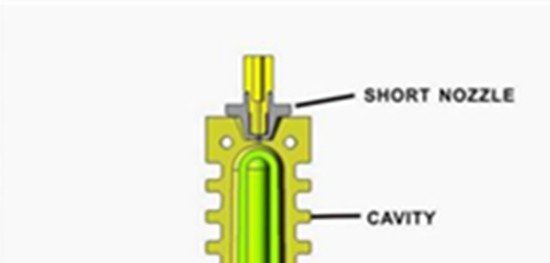
The price of needle valve type is higher than that of self-locking type. It can be seen from the naked eye that the tail of the bottle embryo produced by self-locking type will be longer than that of needle valve type.
The difference between the mold and the finished product can be seen in the following :
Self-locking type mould
The product with self-locking long gate is suitable for the production of large quantities of mid range bottles.
The wall thickness of the bottle embryo is easy to control, which is used to meet no special requirements for the final bottle shape and pursue a solution for mass production.
And the difficulty of mold processing is relatively low, and the price is relatively affordable.
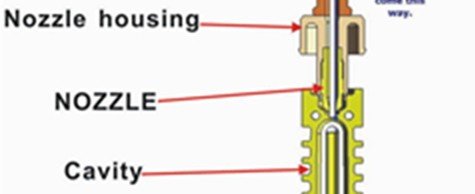
Valve type mould
The product with needle valve gate has a flatter bottle tail and higher accuracy in bottle embryo wall thickness, making it suitable for producing bottles with a better appearance to hold high premium drinks.
Due to the requirement of high precision, the mold is far superior to self-locking in terms of material and processing technology, so the initial cost investment is relatively high.
Machine selection
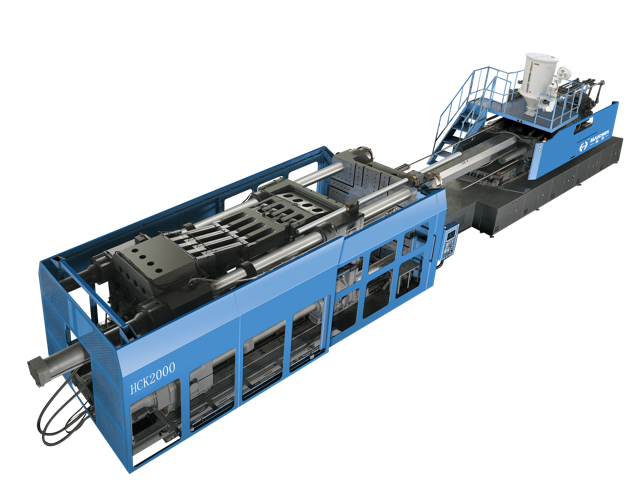
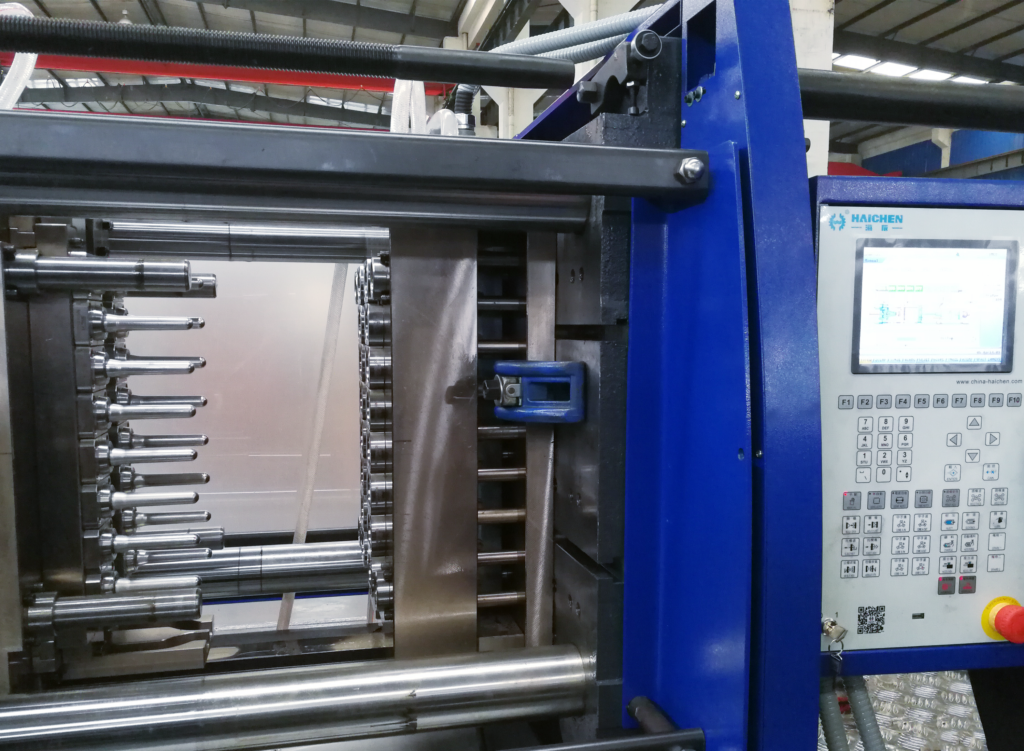
The characteristics of PET materials require machines: PET materials have excellent flowability similar to water when in liquid state, so HCK-PET series machines with specially designed PET injection units must be used in machine selection.
The three main factors for selecting PET bottle embryo machines:
Injection weight
Sapce between four tie bar
Ejection force
Selection of raw materials
PET plastic has excellent thermal sensitivity, so it is necessary to ensure the stable production status of each product, and the mold must use a hot runner form.
And there are extremely high requirements for the matching accuracy of the cavity and core, and the tolerance of product wall thickness must be controlled within a very small range, otherwise unqualified products will have uneven molding or damage during subsequent bottle blowing production.
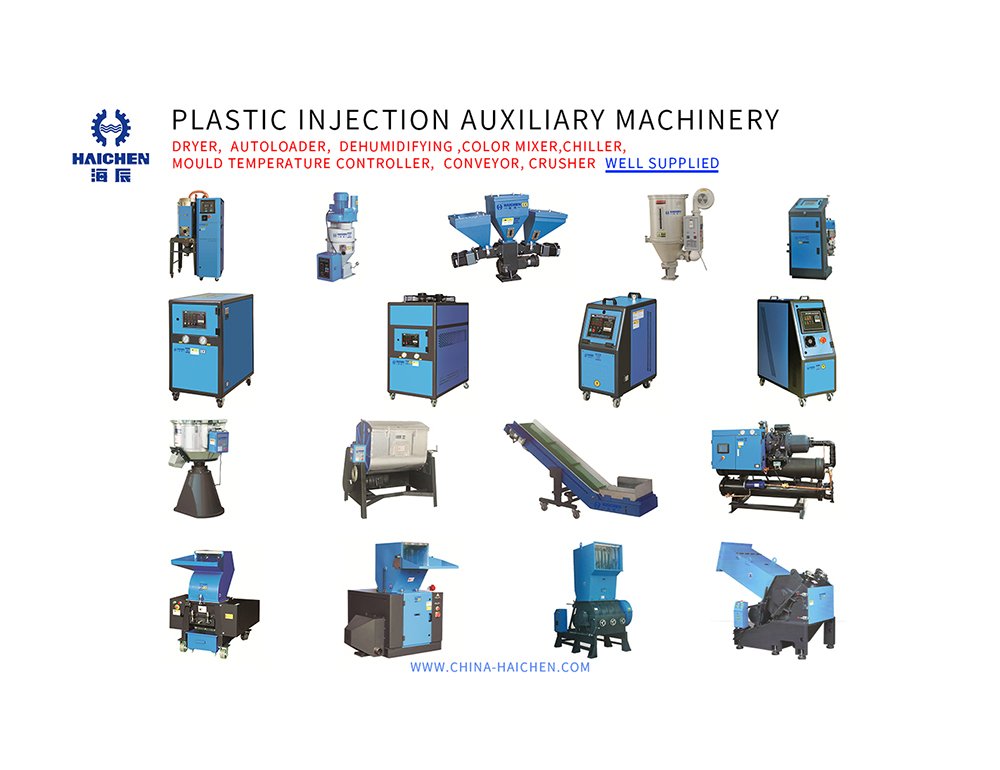
Auxiliary equipment selection
PET raw materials have excellent hydrophilicity and are prone to adsorbing water molecules in natural environments.
Wet raw materials can cause white spots or burnt yellow discoloration during injection molding production, which greatly affects the appearance.
Therefore, before production, the raw materials must be dried using a dryer for 3-5 hours.
In addition, as the bottle embryo mold is a hot runner mold, the production of PET products must accurately control the temperature adjustment of each cycle, so the cooling system is also an essential auxiliary machinery.